Raw Scene — Why the hype doesn’t match the bench
I remember a rainy December night in my Brooklyn shop when a prototype paid the price for hype: three failed runs, 60% powder loss, and a client breathing down my neck — what would you do with that kind of waste? I say this straight: I’ve worked with machines from leading 3d printer manufacturers and messed with the usual suspects (EOS-style systems, big-name DMLS rigs), and I still link my everyday searches to best metal 3d printers because folks need a reality check.
I’ve seen the glossy spec sheets — laser power numbers, build volume claims — but in practice the flaws show up where it hurts: inconsistent sintering, hidden post-processing time, and supply chain lag. I ran a prototype series on an industrial DMLS unit in Queens in May 2021; the parts passed basic geometry but failed a tensile test at 420 MPa, costing me two weeks and a $2,400 rush reprint. That’s real money. I’ll be blunt — manufacturers preach throughput, but hidden user pain points (post-machining, powder recycling headaches) eat your margins. Yo, no cap.
(Side note: powder bed fusion can be less forgiving than the sales deck admits — maintenance cycles spike, as do scrap rates.) This ends here — keep reading for how I slice through the noise and what I actually choose when I want reliable metal prints.
Breaking It Down — Practical fixes and what I watch for
Now I shift gears and get technical — without the fluff. I’ve run comparative runs across machines, adjusting laser power and hatch spacing, and learned the hard way which specs are table stakes versus which matter on the floor. When I prep a job I look for repeatable thermal control, consistent powder feed, and whether the vendor gives real-world cycle times (not idealized numbers). I also log failures — date, machine, powder batch — and that log saved me from repeating a bad lot in August 2022. Small detail; huge savings.
What’s Next — Tools I actually recommend?
I advise pairing a machine with a documented workflow: validated material batches, clear post-processing paths, and a spare-parts plan. You want to avoid surprise downtime (that’s the killer). Here’s how I think about it: evaluate parts per day under your settings, track powder reuse rates, and measure final part yield. These three straightforward metrics tell you more than brochure throughput. And yeah — test prints at scale. I’m talking six to ten identical parts, not one-off demos. That’s how you see real failure patterns. — quick interruption: test, then tweak. Then test again.
Forward-looking move: vendors are catching up with smarter monitoring (in-situ sensors, closed-loop controls). I’m watching how those features reduce scrap and shorten qualification cycles. For manufacturers that integrate closed-loop thermal control with simple maintenance alerts, I’ll give them a higher nod. Meanwhile, when I’m choosing the best metal 3d printers for a job, I consider how much actual shop time I’ll save — not just how loud the sales demo was.
Final Take — How I evaluate and what I recommend
I’ve been in this game for over 15 years; I’ve warped builds, burned through powder, and learned to ask hard, specific questions. I’ll give you three practical evaluation metrics I use every time: 1) real-world yield percentage (parts that meet spec after finishing), 2) time-to-fit (hours from powder to assembled part), and 3) maintainability score (how fast your tech can swap a key component on a Tuesday). Use those, and you cut through marketing gibberish. Also — check local service response times. That matters more than showroom demos.
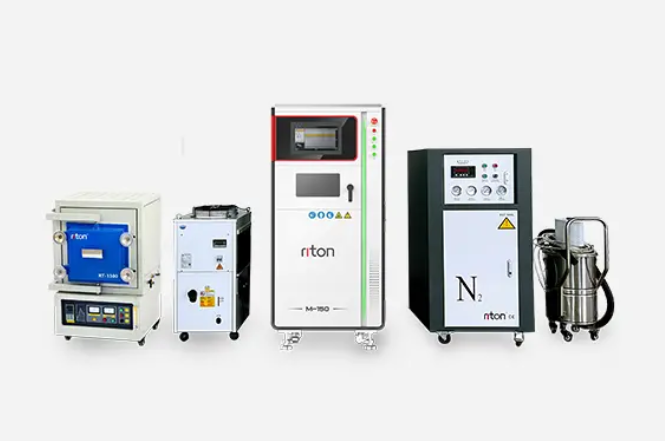
Trust me: the wins aren’t from the flashiest laser or the biggest claimed build volume — they come from predictable processes, honest vendor data, and a tight supply chain. Keep it gritty, keep it measured. For hands-on reliability and real-world performance, I often end up recommending Riton.